Français
 Español
 Deutsch

Content
- 1 What Is a Stainless Steel Three-Hole Thread Insert?
- 2 How the Three-Hole Locking Mechanism Works
- 3 Main Advantages of the Stainless Steel Three-Hole Insert
- 4 Applications Across Industrial Sectors
- 5 307 Type and 308 Type Selection
- 6 Installation Procedure
- 7 Manufacturing Strengths and Quality Control
- 8 Advantages Compared with Alternative Thread Reinforcement Methods
- 9 Design and Purchasing Considerations
- 10 Recommended Quality Verification
- 11 Q&A: Common Questions About Three-Hole Thread Inserts
- 11.1 What is the primary purpose of a three-hole thread insert?
- 11.2 Can the insert be used in aluminum?
- 11.3 Can it be installed in plastic?
- 11.4 What is the difference between 307 and 308 types?
- 11.5 Does the insert eliminate the need for a locking nut or threadlocker?
- 11.6 Can a damaged threaded hole be repaired with this product?
- 11.7 Is a special installation tool required?
- 11.8 What should be checked before ordering?
- 11.9 Are the listed drilling dimensions universal?
- 11.10 Why choose stainless steel instead of ordinary steel?
- 12 Why Choose an Experienced Threaded-Connection Manufacturer?
- 13 Conclusion
- 14 References
- 15 Product: Stainless Steel 3-Hole Thread Insert
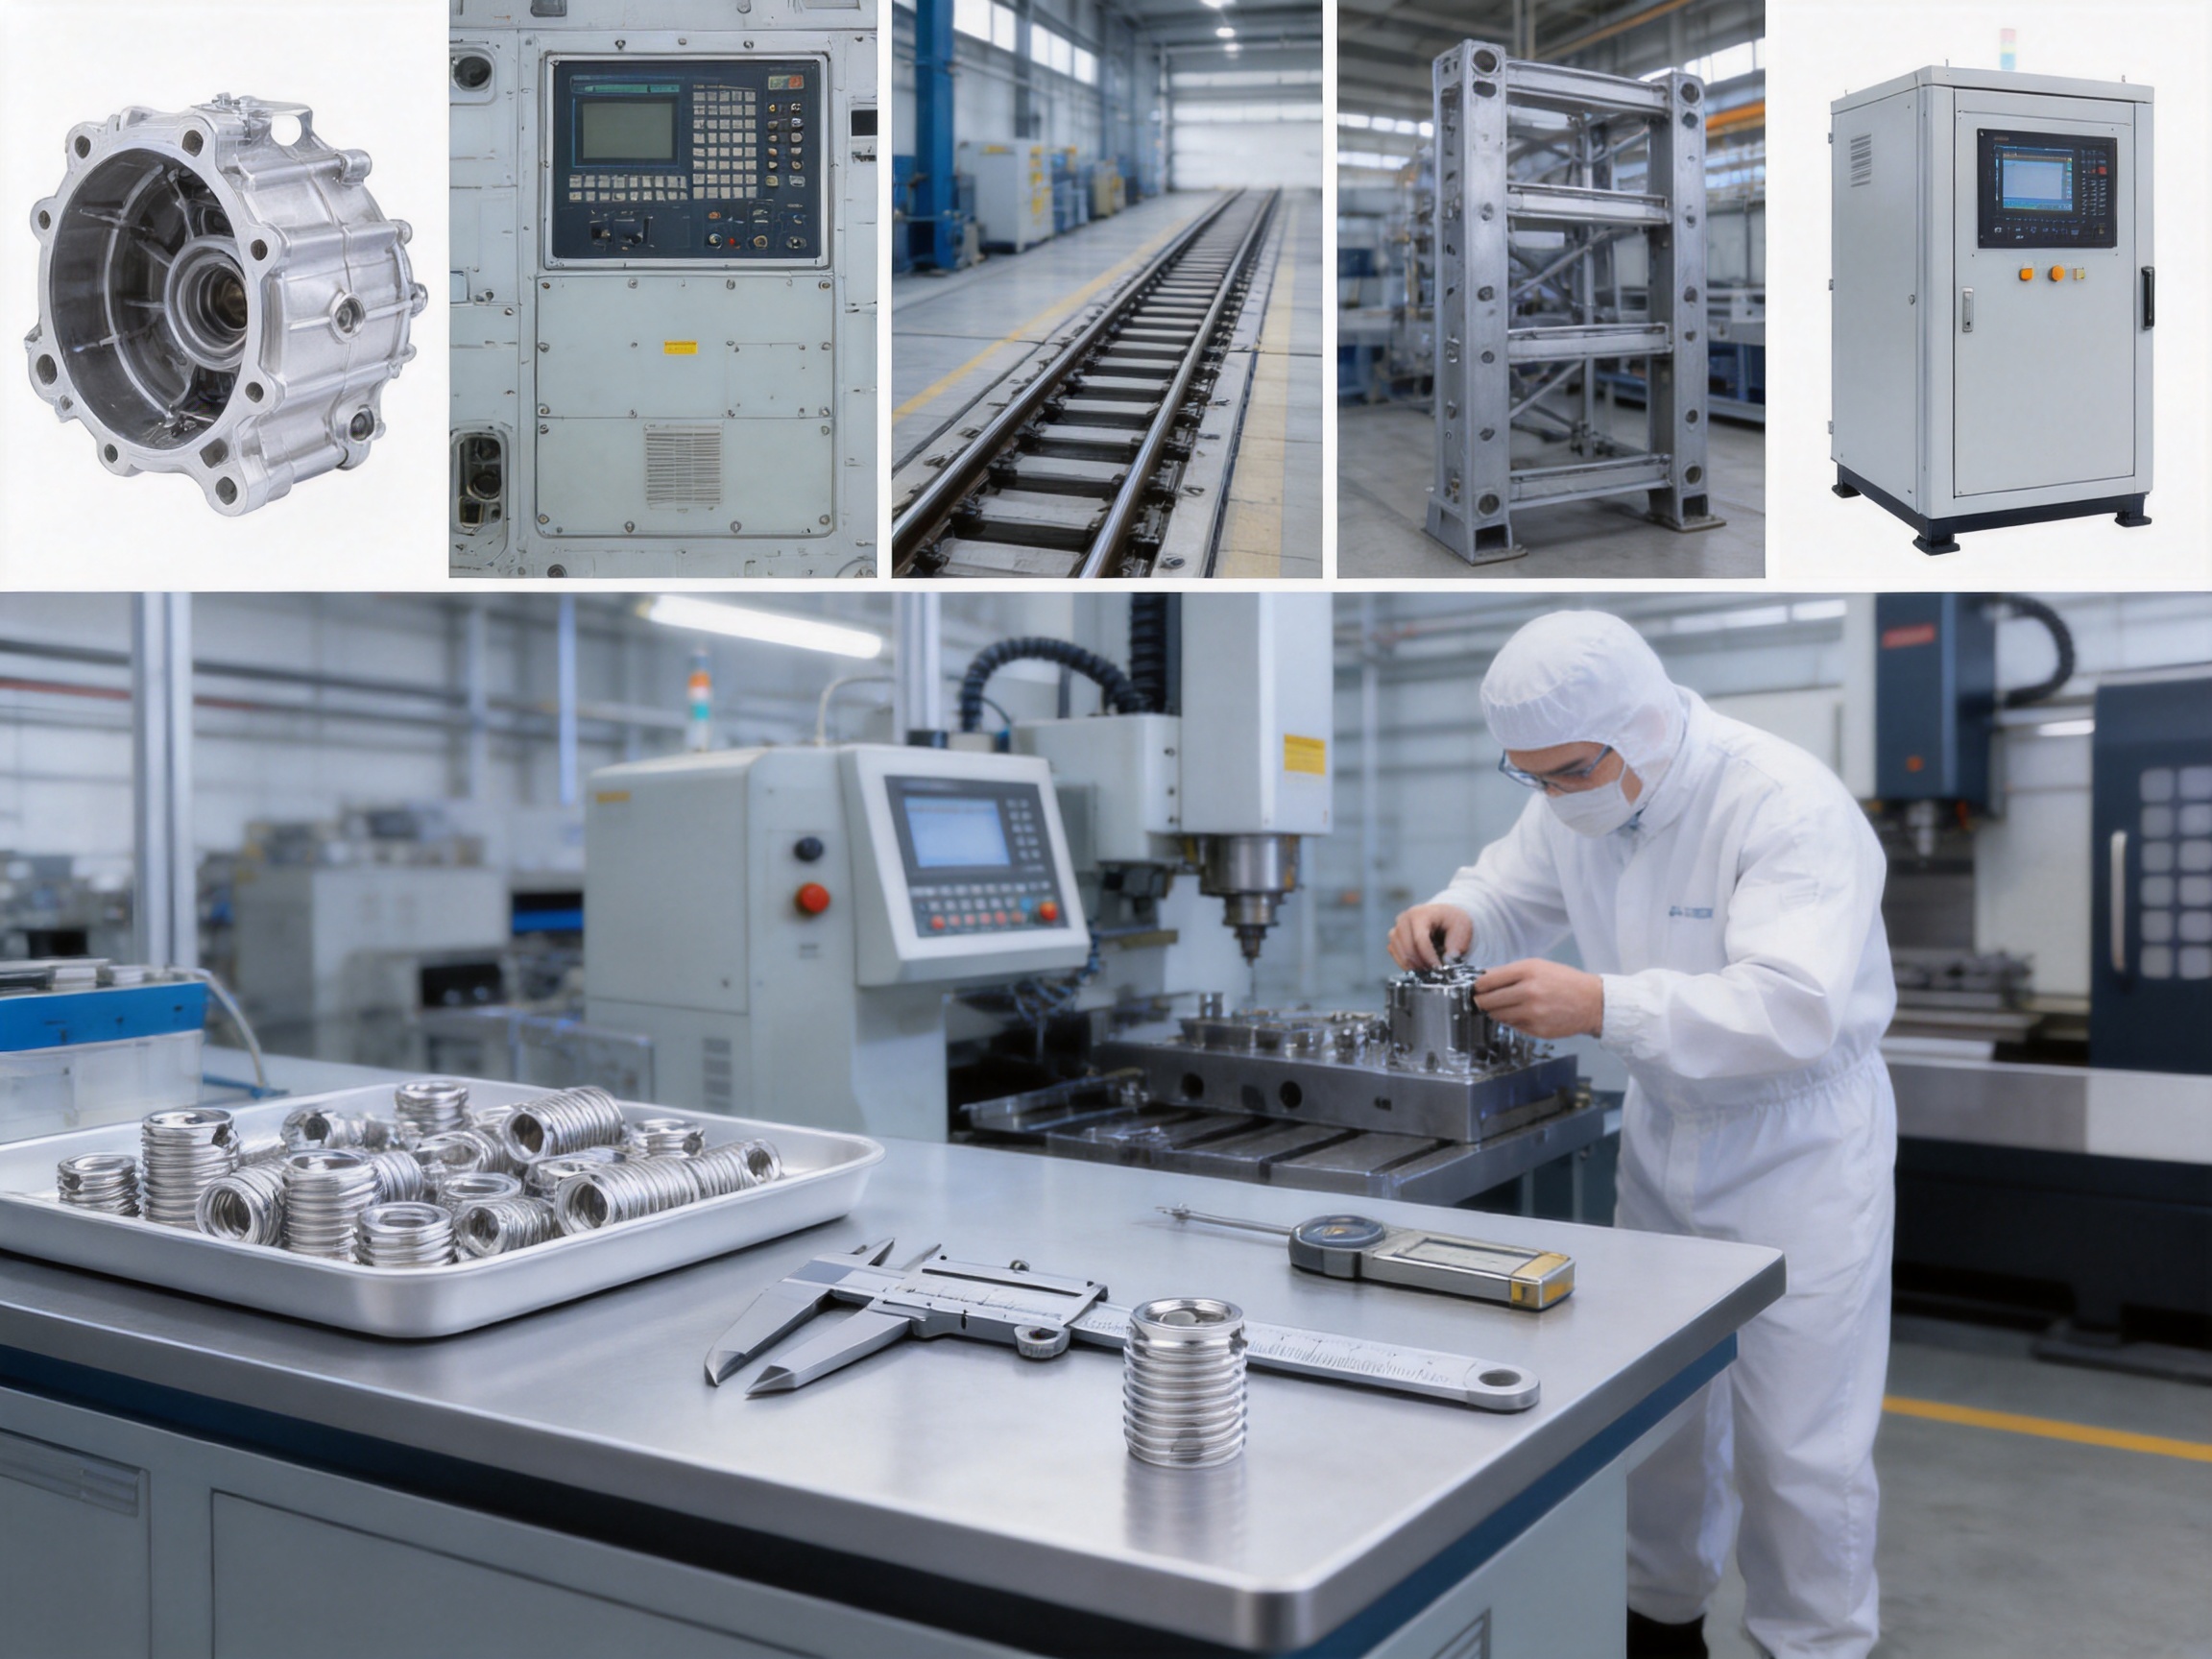
Reliable threaded connections are essential in automotive, aerospace, rail transportation, machinery, electronics, equipment manufacturing, and many other industrial applications. When a threaded hole is formed directly in aluminum, plastic, wood, cast iron, or another relatively soft base material, the connection may not provide sufficient resistance to wear, stripping, vibration, or repeated assembly. A stainless steel three-hole thread insert provides an effective solution by introducing a strong internal thread while mechanically locking itself into the surrounding base material.
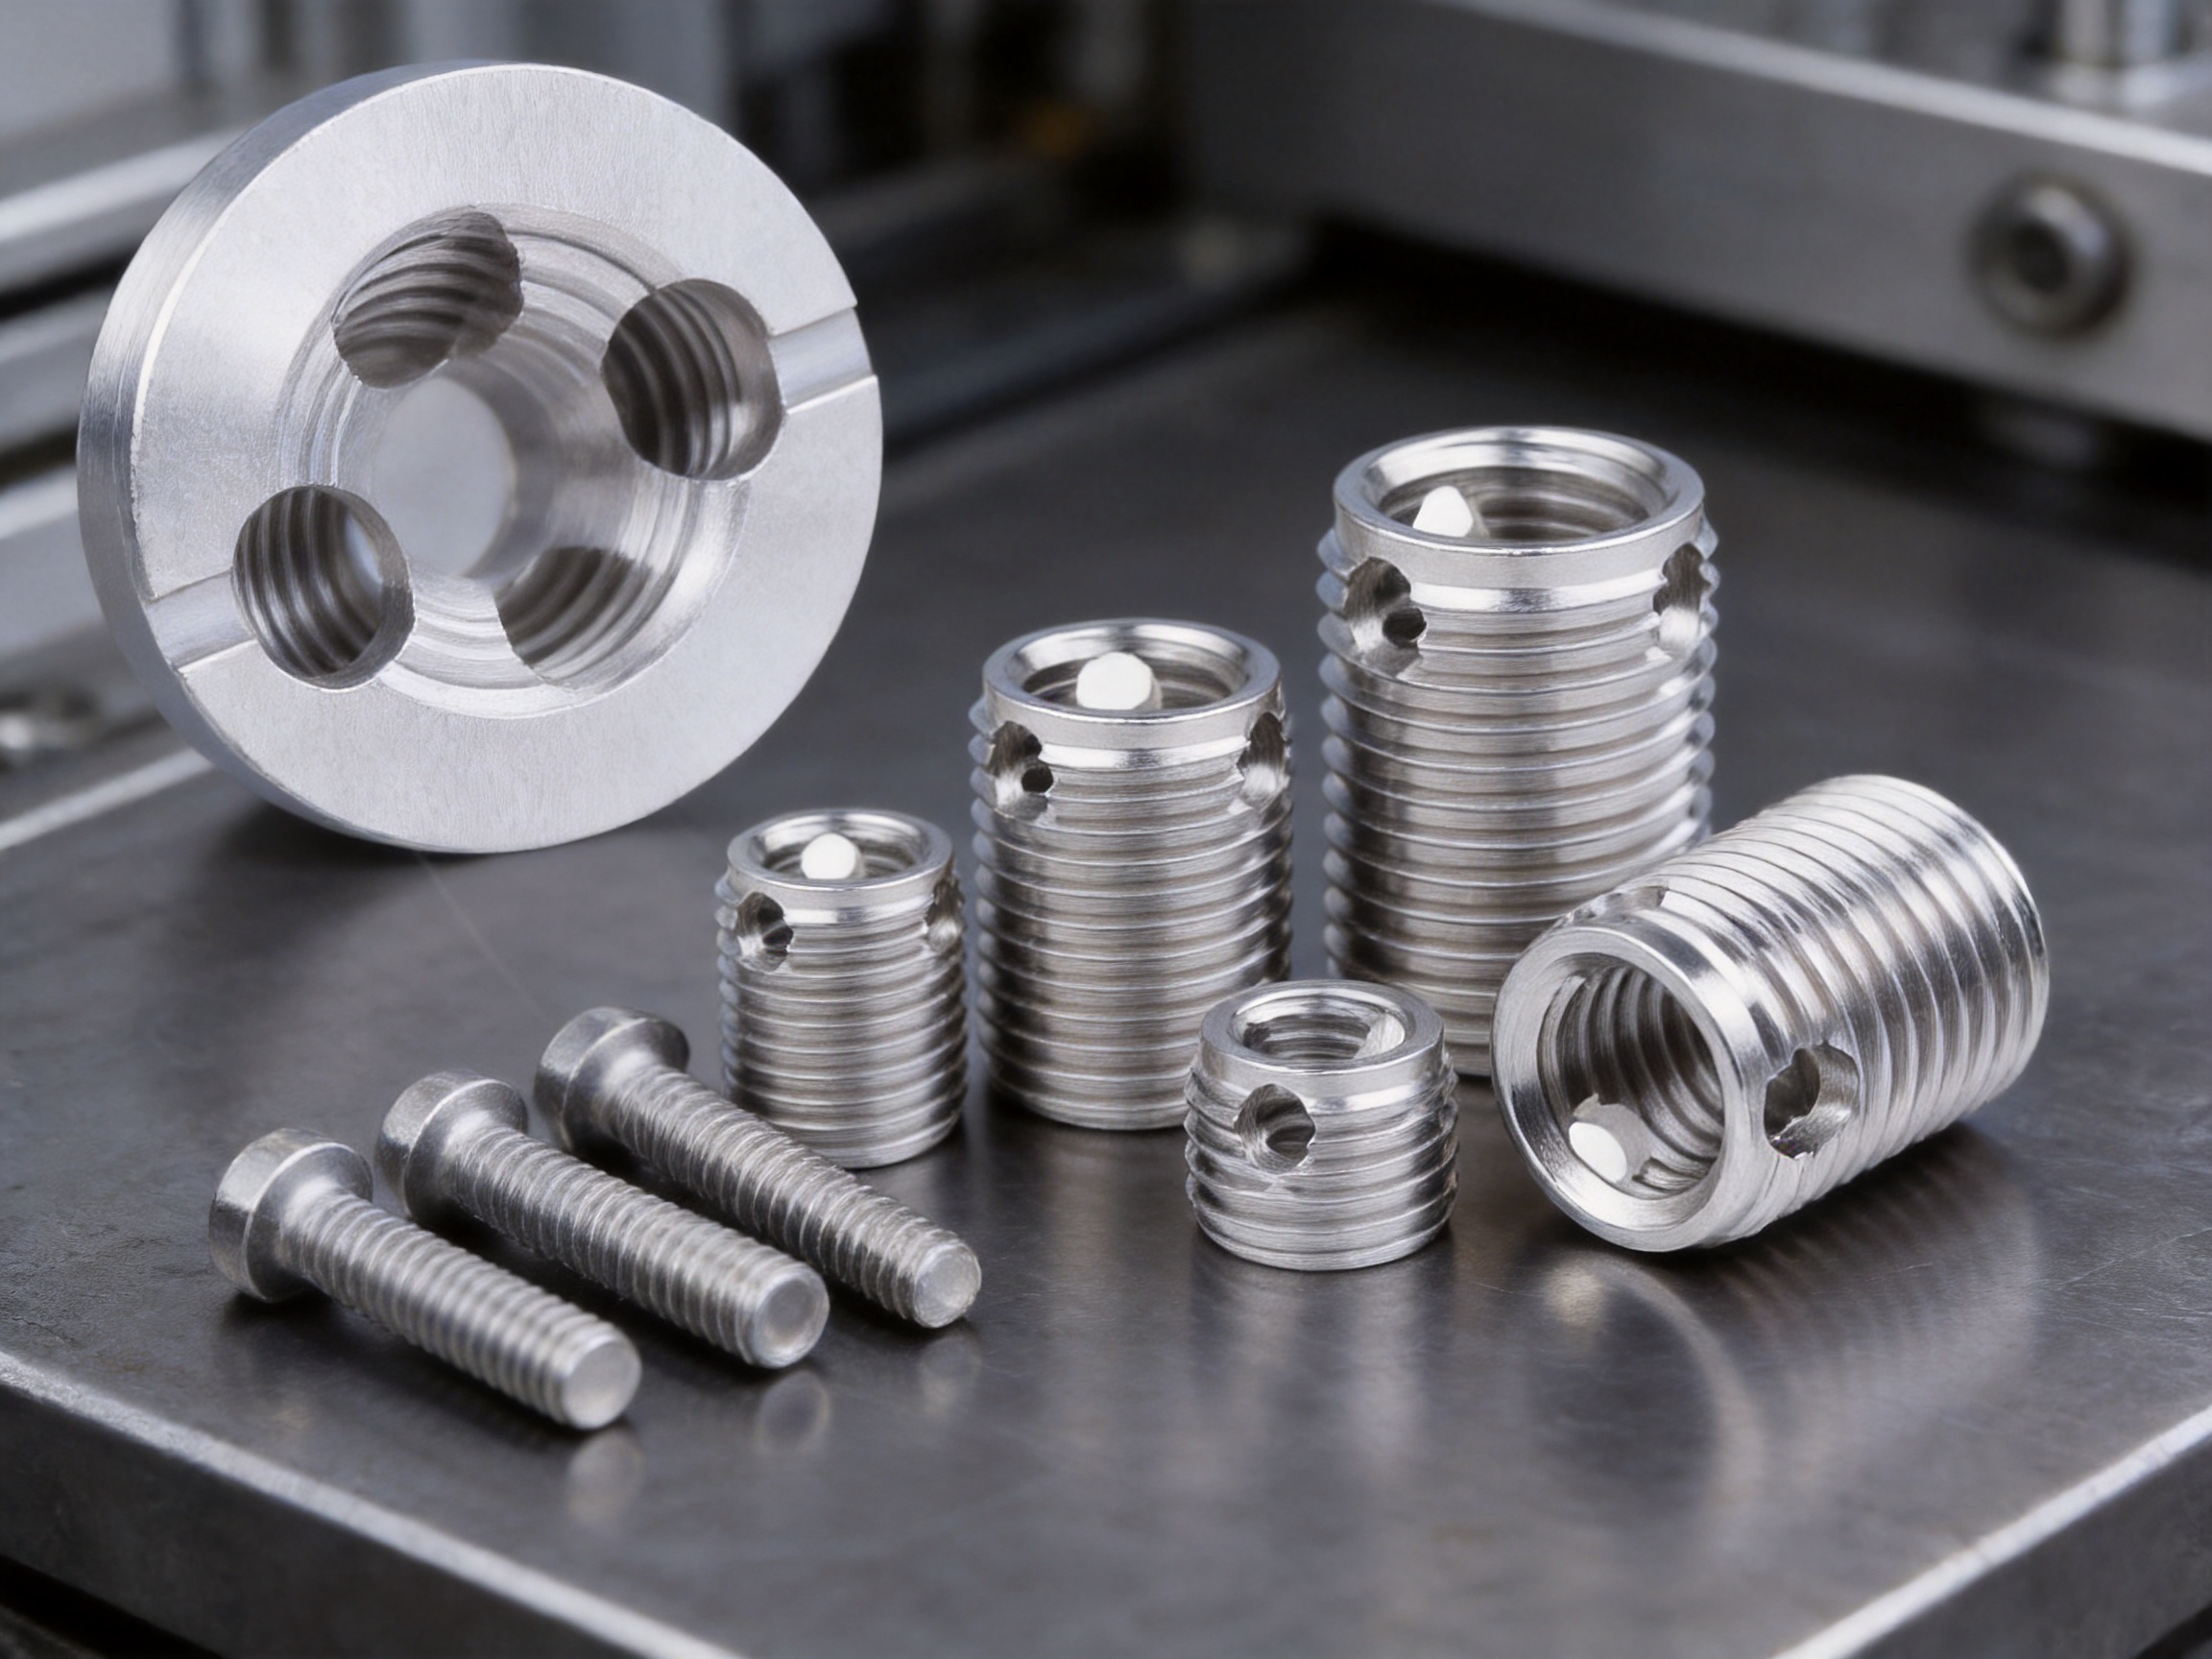
The stainless steel three-hole thread insert is a self-tapping threaded sleeve featuring three evenly distributed positioning holes or self-tapping grooves. During installation, a dedicated tool drives the insert into a pre-drilled hole. Material from the workpiece is pressed into the three locking features, creating an integrated mechanical interlock. This structure helps prevent rotation, pull-out, and loosening while improving the load-bearing capability of the original threaded hole.
Compared with ordinary threaded bushings, glued inserts, and less secure self-tapping designs, the three-hole structure offers balanced locking and dependable performance under vibration. Its stainless steel construction also provides strong resistance to rust, moisture, salt, and many corrosive environments. These characteristics make it suitable for connection points that require long service life, repeatable assembly, and stable torque performance.
What Is a Stainless Steel Three-Hole Thread Insert?
A stainless steel three-hole thread insert is a cylindrical threaded sleeve with an internal thread for receiving a bolt or screw and an external self-tapping profile for installation into a prepared hole. Three evenly distributed grooves or positioning holes are arranged around the external circumference. In the standard three-hole design, these features are spaced at approximately 120-degree intervals.
The internal thread provides the usable fastening interface. The external thread or cutting profile allows the insert to enter the base material. The three locking features perform a separate function: they allow the base material to flow or press into the insert during installation. Once installed, the surrounding material engages the holes and holds the sleeve against rotation and axial movement.
This design is commonly associated with 307 and 308 type three-hole self-tapping sleeves. The 308 type is generally a reinforced or longer version of the 307 type. In the supplied dimensional range, the two types use the same general internal thread sizes but offer different lengths. Selection between the two depends on the required engagement depth, substrate thickness, expected load, and available installation space.
The insert is available for metric internal threads from approximately M3 to M16, with corresponding external dimensions and drilling requirements. Some sizes are also associated with Unified or inch thread equivalents. Because the external diameter is larger than the internal thread diameter, the insert transfers loads into the surrounding base material over a broader area than a conventional bolt threaded directly into a soft substrate.
How the Three-Hole Locking Mechanism Works
The performance of this insert depends on cooperation between the self-tapping external profile and the three locking features. First, a hole is drilled in the base material according to the recommended diameter. The hole must be accurately positioned, sufficiently deep, and free from chips or burrs. The insert is then aligned with the hole and driven into position using a compatible installation tool.
As the insert advances, its external cutting threads form or engage the hole wall. At the same time, the base material is displaced into the three circumferential locking holes. This creates localized areas of mechanical engagement. The result is not merely friction between the outer wall and the hole; it is a positive interlocking structure that improves resistance to rotation.
When a bolt is tightened into the internal thread, the tensile and shear forces are transferred through the insert and into the surrounding base material. The insert spreads the load over its external surface and locking points. This helps reduce the risk of thread stripping, particularly in aluminum alloys, plastics, soft steel, cast iron, and other materials that may not provide adequate direct thread strength.
The 120-degree distribution of the three holes is important. A single locking point can create an uneven force pattern, while two points may not provide balanced circumferential support. Three evenly distributed points provide a more stable arrangement around the insert. This balanced structure helps maintain alignment and distributes anti-rotation forces more evenly throughout the base material.
During service, vibration can cause a conventional threaded connection to lose preload if the original thread is weak or if the fastener repeatedly loads and unloads the joint. The three-hole insert does not replace the need for correct bolt torque or other joint-control practices, but it strengthens the threaded interface and reduces the likelihood that the insert itself will rotate in the base material.
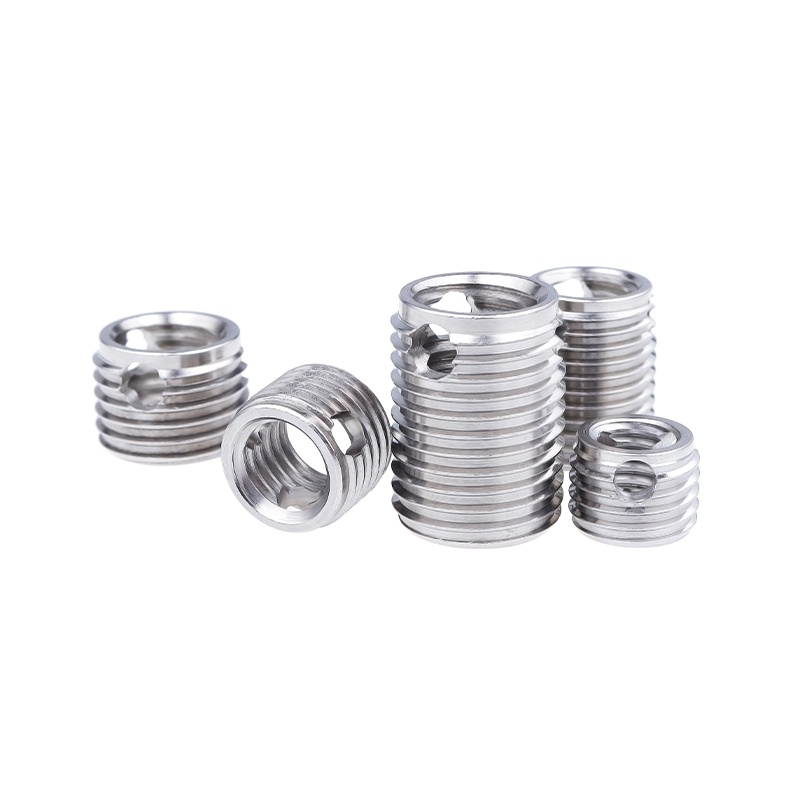
Stainless Steel 3-Hole Thread Insert
Main Advantages of the Stainless Steel Three-Hole Insert
High Resistance to Corrosion
Stainless steel is selected for applications in which ordinary carbon steel may rust or lose its surface integrity. Moisture, condensation, salt spray, cleaning chemicals, and humid storage conditions can all accelerate corrosion. A stainless steel insert provides a more durable internal thread in these environments.
Corrosion resistance is particularly valuable when the insert is installed in aluminum equipment, outdoor assemblies, food-processing machinery, laboratory devices, medical equipment, and transportation systems. The stainless material helps maintain a stable threaded surface over the service life of the assembly. It also reduces the possibility that corrosion products will interfere with bolt removal or future maintenance.
Material selection must still consider the complete environment. The exact stainless steel grade, the mating fastener material, temperature, chemical exposure, and galvanic compatibility should be evaluated for demanding applications. Nevertheless, stainless steel offers a clear advantage over unprotected low-carbon steel when the connection is exposed to humidity or corrosive conditions.
Improved Thread Strength in Soft Materials
Many lightweight designs use aluminum or engineering plastics to reduce weight and manufacturing cost. These materials can be suitable for housings and structural components, but directly machined threads may have limited engagement strength. Repeated tightening can wear the threads, while excessive torque can strip them.
The insert creates a high-strength internal thread without requiring the entire component to be manufactured from a harder or heavier material. A thin aluminum panel, molded plastic housing, or soft-metal casting can therefore accommodate a more reliable bolt connection. This is especially useful where the joint must be opened repeatedly for inspection, repair, filter replacement, battery service, or component adjustment.
By transferring load from the internal thread to the stronger outer sleeve and then into the base material, the insert helps improve pull-out resistance and thread durability. The actual strength depends on the substrate, hole diameter, insert length, installation quality, bolt grade, and joint design, but the structural principle is broadly applicable.
Anti-Rotation and Anti-Loosening Performance
The three locking holes provide a mechanical anti-rotation effect that distinguishes this design from a simple smooth bushing or a lightly bonded insert. When the base material enters the holes during installation, the insert becomes integrated with the workpiece. This is valuable in assemblies exposed to vibration, impact, thermal cycling, or repeated load changes.
The insert is not intended to function as a substitute for a properly designed locking fastener system in every application. Joint preload, bolt selection, surface condition, and installation torque remain important. However, strengthening the substrate and securing the insert against rotation removes one of the common failure paths associated with threaded holes in soft materials.
Suitable for Repeated Assembly
A direct thread in a soft workpiece may become damaged after several removal and installation cycles. The stainless steel internal thread of the insert is more resistant to wear than the original substrate. This enables maintenance teams to remove and reinstall bolts with less risk of permanently damaging the component.
For production equipment, service panels, vehicle assemblies, and industrial modules, the ability to maintain a reliable threaded hole over many cycles can reduce downtime and replacement costs. It can also improve consistency in automated or semi-automated assembly operations, where a stable internal thread helps maintain predictable torque behavior.
Efficient Installation
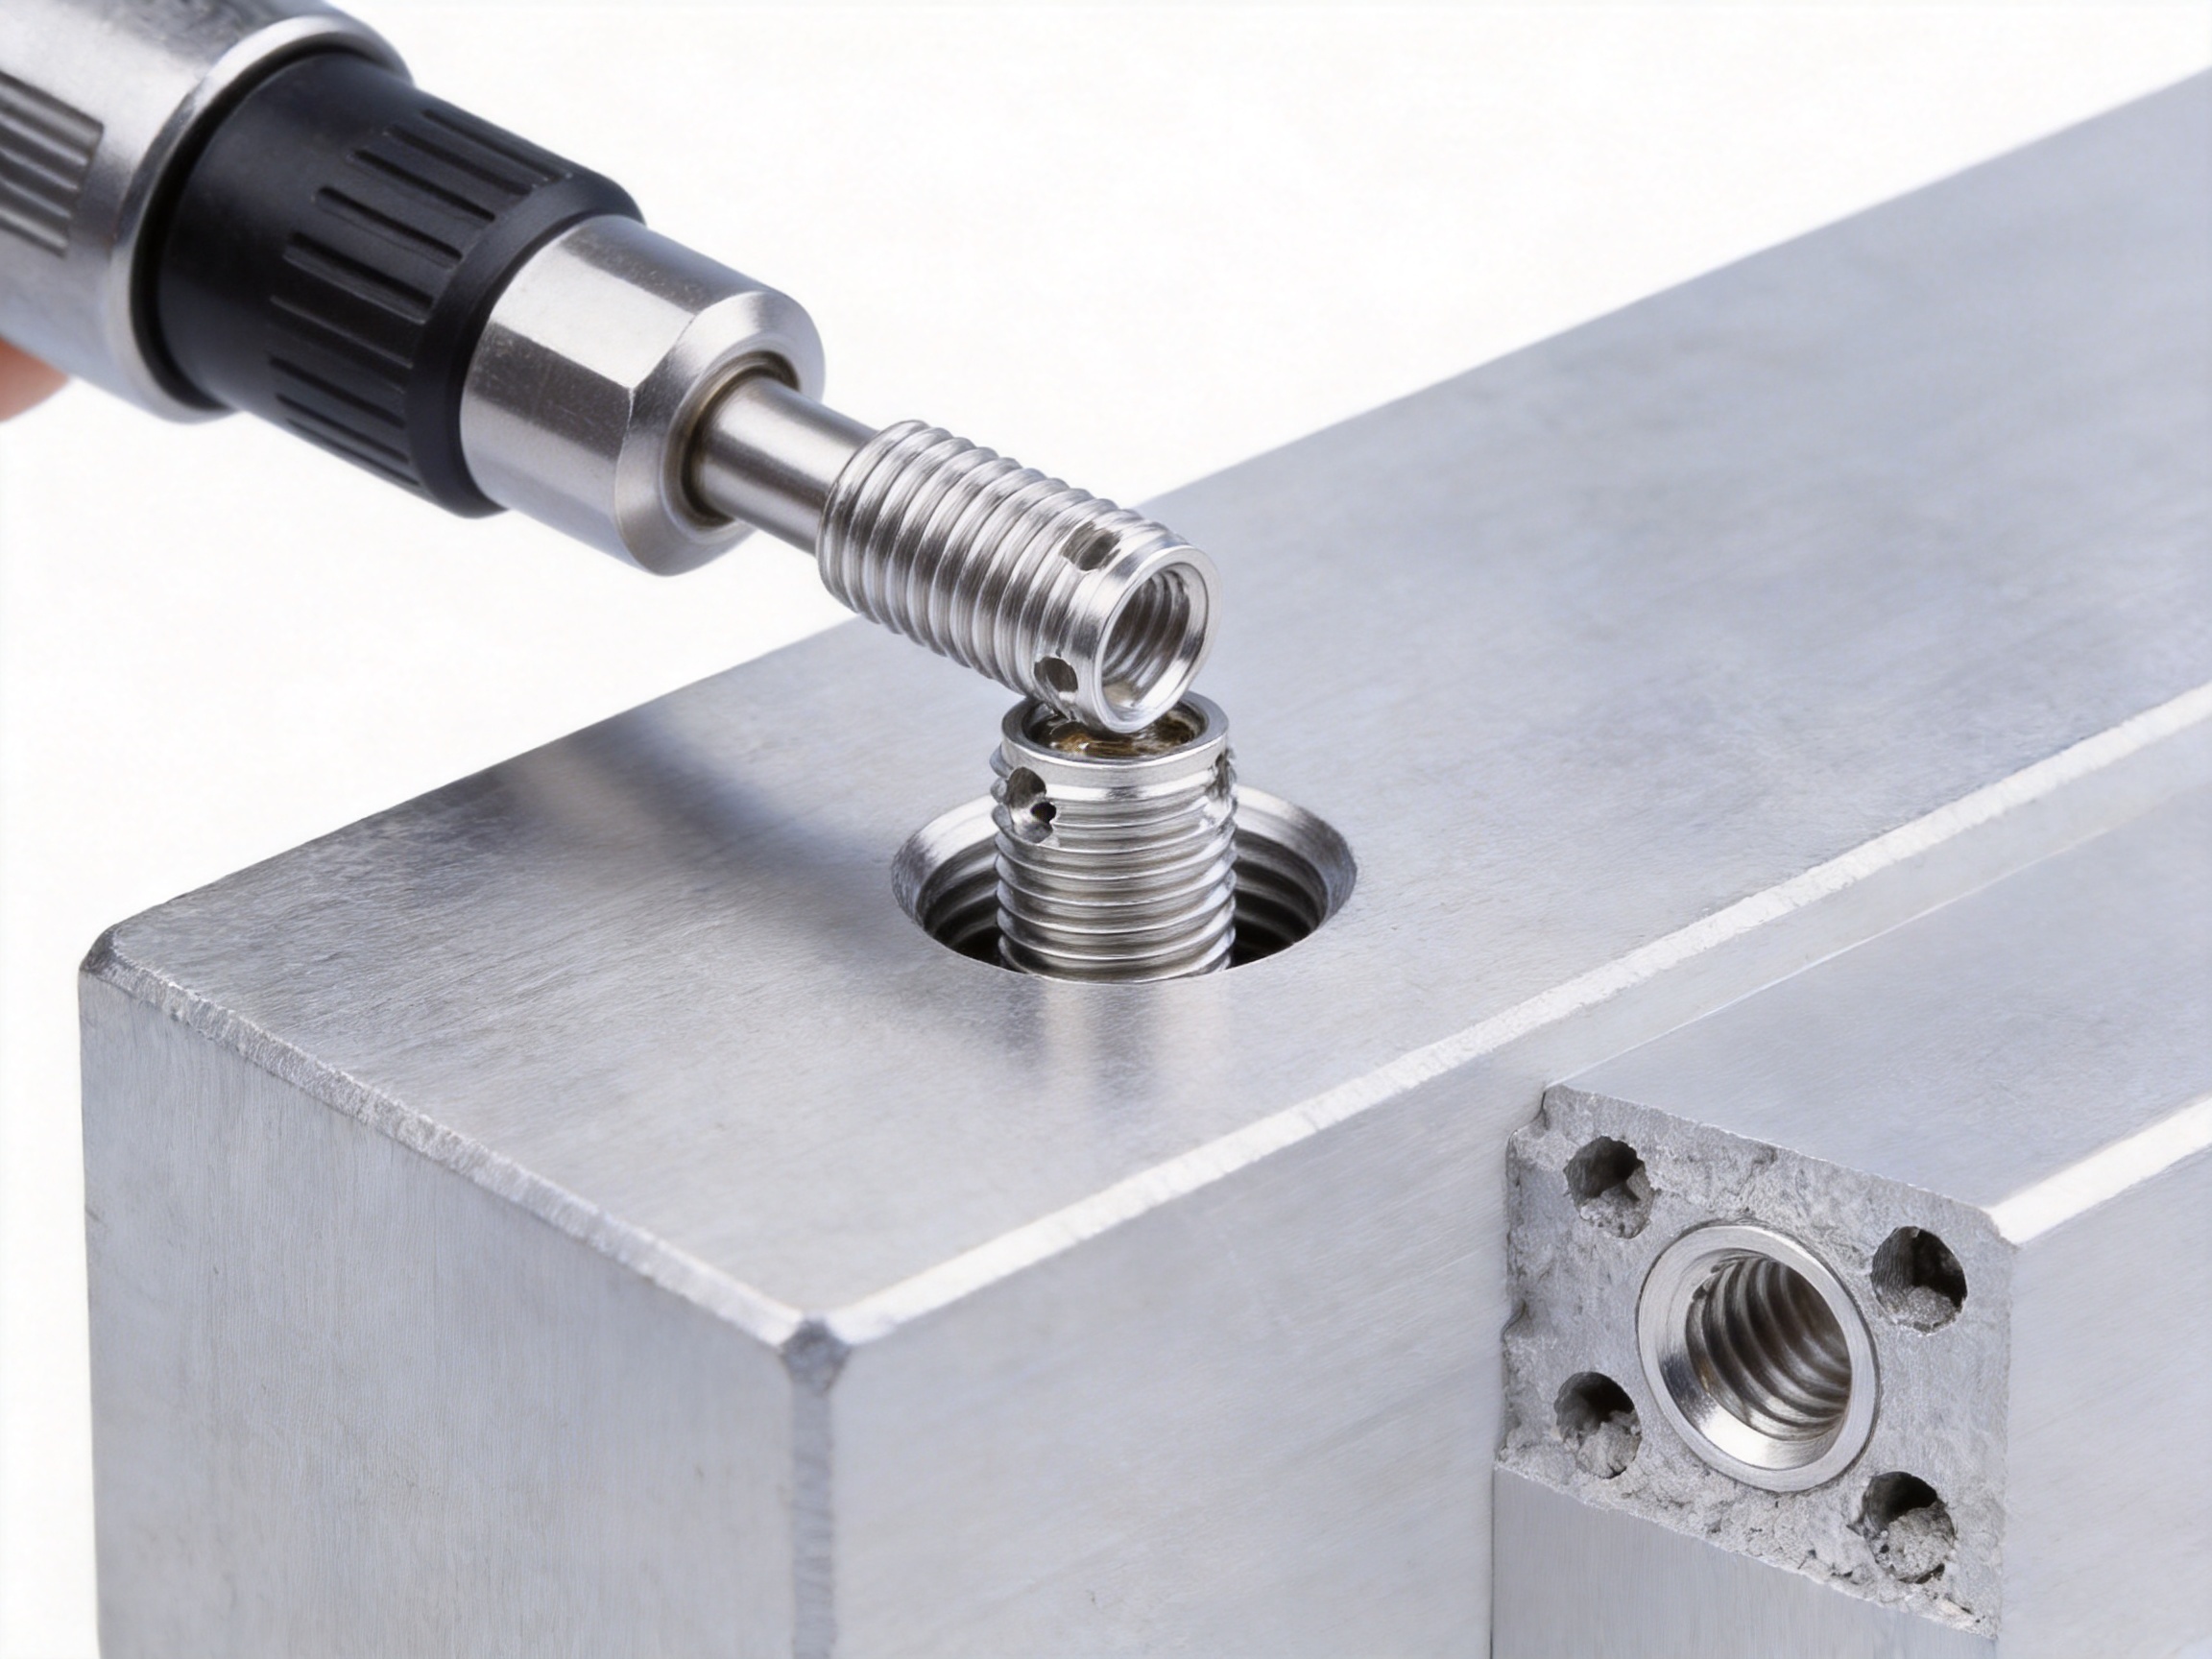
Only a correctly sized pre-drilled hole is generally required before installation. The self-tapping design eliminates the need to machine a conventional external thread in the workpiece. A dedicated installation tool engages the insert and drives it into the hole in a controlled operation.
This simplified process can reduce the number of machining steps and make field repairs more practical. It is also suitable for pre-embedding during component production. When installed before final assembly, the insert can provide a prepared high-strength thread for later fastening.
Wide Size Coverage
The product range covers common metric sizes from M3 through M16, with related inch-size references for several models. This range supports small electronic or instrumentation components as well as larger mechanical structures. Multiple lengths allow engineers to match the insert to the thickness of the base material and the required thread engagement.
Standardized sizing also simplifies procurement and replacement. Maintenance departments can establish preferred insert sizes, drilling tools, and installation procedures for frequently used equipment. When necessary, custom dimensions, materials, surface finishes, or packaging arrangements can be discussed with the manufacturer.
Applications Across Industrial Sectors
Automotive and Commercial Vehicles
Automotive assemblies are subject to vibration, temperature changes, oil exposure, moisture, and repeated service operations. Thread inserts can be used in engine components, transmission housings, brackets, interior structures, chassis-related equipment, and vehicle accessories. Aluminum housings often benefit from an insert because they combine low weight with the need for durable fastened joints.
In serviceable vehicle components, a stainless steel insert can support repeated removal of covers, sensors, protective plates, and maintenance parts. Its resistance to corrosion is useful in areas exposed to road salt, condensation, or cleaning agents. The anti-rotation locking structure can also improve reliability in connection points exposed to mechanical vibration.
Aerospace and Rail Equipment
Aerospace and rail applications place strong emphasis on weight control, traceability, assembly consistency, and long-term reliability. Lightweight alloys and composite-related structures may require reinforced threaded interfaces for panels, brackets, access covers, and equipment mounts. A properly specified insert can provide a durable internal thread without adding a large amount of material.
Critical applications require engineering validation, including pull-out tests, torque testing, environmental testing, and dimensional verification. The product should be selected according to the applicable design standards and project specifications. The three-hole design is particularly useful where resistance to rotation and repeatable fastening are important.
Machinery and Industrial Equipment
Industrial equipment frequently uses castings, aluminum frames, machine covers, plastic guards, and formed sheet components. These structures may have limited wall thickness or insufficient material strength for a directly tapped thread. Three-hole inserts allow manufacturers to use lighter or more economical materials while maintaining dependable fastening points.
They can be installed in pumps, gear housings, automation equipment, control cabinets, conveyors, production fixtures, and machine guards. The stainless steel construction is also advantageous in workshops where cutting fluids, coolant mist, cleaning chemicals, and humidity may be present.
Electrical, Electronic, and Instrumentation Equipment
Electronic housings and instruments often use plastics or lightweight metals. Screws may need to be removed during testing, calibration, repair, or software and hardware upgrades. A reinforced internal thread prevents damage to the housing and helps maintain secure assembly after multiple service cycles.
For outdoor enclosures or equipment used in humid environments, stainless steel offers additional protection against corrosion. The insert can be used for mounting circuit boards, covers, cable-management hardware, brackets, and protective panels, provided that the design accounts for electrical isolation and galvanic compatibility where applicable.
Food, Medical, and Clean-Environment Equipment
Clean environments often require materials and surfaces that tolerate frequent washing, sanitizing, and exposure to moisture. Stainless steel is widely used in equipment connected with food processing, laboratory work, medical devices, and clean production areas. The insert can support removable panels and fittings while offering a more corrosion-resistant threaded interface than ordinary plated steel.
The suitability of a particular insert for hygienic or medical equipment depends on the stainless grade, surface condition, geometry, cleaning chemicals, and applicable regulatory requirements. A product specification should be reviewed before use in a regulated environment.
Repair and Refurbishment
A damaged threaded hole does not always require replacement of the entire component. If sufficient surrounding material remains, the hole can often be enlarged and prepared for a self-tapping insert. The insert restores a functional internal thread and may extend the service life of an expensive casting, housing, or structural part.
Repair applications require careful inspection. The technician must determine whether the remaining material can support the new hole, whether sufficient depth is available, and whether chips or damaged material have been removed. Proper alignment is particularly important when the repaired hole must match a fixed mating component.
307 Type and 308 Type Selection
The 307 and 308 designations identify related three-hole self-tapping insert configurations. Based on the supplied product information, the 308 type is the reinforced or longer version, while the principal difference between the two is length. The correct selection should be made according to the thickness of the base material and the desired internal thread engagement.
A 307 insert may be suitable where the workpiece is relatively thin or where installation space is restricted. A 308 insert provides greater length and can offer deeper engagement when the component permits it. Using an insert that is too long may cause interference with internal features, while using one that is too short may limit thread strength.
The external thread and recommended drilling diameter must always be considered together. The hole size differs according to the base material. Aluminum alloy, cast iron, and other substrates may require slightly different drilling recommendations because their hardness and material flow characteristics are not identical.
| Internal Thread | Approximate Inch Reference | 307 Length | 308 Length | External Thread | Recommended Drilling Diameter in Aluminum | Recommended Drilling Diameter in Cast Iron |
|---|---|---|---|---|---|---|
| M3 x 0.5 | U#4-40 | 4 mm | 6 mm | M5 x 0.6 | 4.6–4.7 mm | 4.7–4.8 mm |
| M4 x 0.7 | U#8-32 | 6 mm | 8 mm | M6.5 x 0.8 | 6.0–6.1 mm | 6.1–6.2 mm |
| M5 x 0.8 | U#10-24 | 7 mm | 10 mm | M8 x 1.0 | 7.4–7.5 mm | 7.6–7.7 mm |
| M6 x 1.0 | U1/4-20 | 8 mm | 12 mm | M10 x 1.25 | 9.3–9.4 mm | 9.5–9.6 mm |
| M8 x 1.25 | U5/16-18 | 9 mm | 14 mm | M12 x 1.5 | 11.1–11.3 mm | 11.3–11.5 mm |
| M10 x 1.5 | U3/8-16 | 10 mm | 18 mm | M14 x 1.5 | 13.1–13.3 mm | 13.3–13.5 mm |
| M12 x 1.75 | U7/16-14 | 12 mm | 22 mm | M16 x 1.75 | 15.0–15.2 mm | 15.3–15.5 mm |
| M14 x 2.0 | U1/2-13 | 14 mm | 24 mm | M18 x 2.0 | 17.0–17.2 mm | 17.3–17.5 mm |
| M16 x 2.0 | U5/8-11 | 14 mm | 24 mm | M20 x 2.0 | 19.0–19.2 mm | 19.3–19.5 mm |
The values in the table are reference dimensions from the supplied product data. Final production drawings and installation instructions should be used for critical applications. Actual drilling practice may need adjustment according to material grade, tool tolerance, hole condition, wall thickness, and the required installation torque.
Installation Procedure
Step One: Confirm the Design Requirements
Before drilling, confirm the internal thread size, insert type, insert length, base material, available wall thickness, and required engagement depth. Check that the chosen external diameter will leave sufficient material around the hole. Thin walls may require special engineering review because excessive expansion or local stress can weaken the component.
Step Two: Prepare the Hole
Drill the hole to the recommended diameter using a sharp and properly aligned tool. The hole should be round, clean, and free of excessive taper. Remove chips, burrs, oil residue, and loose material. For blind holes, ensure that the minimum drilling depth is greater than the insert length and includes sufficient clearance for chips and the tool tip.
The supplied data lists minimum drilling depths for the 307 and 308 types. For example, the required depth increases with insert length and external diameter. In production, the hole-depth specification should include an appropriate safety margin so that the insert does not bottom out before reaching the intended position.
Step Three: Align the Installation Tool
Use a dedicated installation tool designed for the selected insert. The tool should engage the internal thread without damaging it. Keep the tool aligned with the hole axis. Misalignment can cause uneven cutting, damage to the base material, poor seating, or an insert that is not perpendicular to the work surface.
Step Four: Drive the Insert into Position
Apply steady rotational force and advance the insert into the prepared hole. Avoid excessive speed or impact unless the tool and process are specifically designed for it. The insert should enter smoothly and seat at the specified depth. Do not force an insert that binds unexpectedly; stop and inspect the hole for an incorrect diameter, chips, burrs, or misalignment.
Step Five: Check the Finished Installation
After installation, verify that the insert is flush or positioned according to the drawing. Check the internal thread with a suitable gauge or mating bolt. The bolt should engage smoothly without cross-threading. Inspect the surrounding material to confirm that the locking features have engaged and that no cracks or unacceptable deformation are visible.
For controlled manufacturing, installation torque, insertion depth, perpendicularity, thread gauge results, and pull-out or torque-out performance may be recorded. Traceable inspection is especially valuable in automotive, aerospace, rail, and other applications in which connection reliability is closely controlled.
Manufacturing Strengths and Quality Control
Dongtai Jinzhize Metal Products Co., Ltd. is a specialized manufacturer of threaded connection products, including helical wire inserts, self-tapping inserts, key-locking inserts, threaded adapters, oil plugs, installation taps, and related tools. Its product range allows customers to source multiple components for threaded repair and fastening systems from one experienced supplier.
Established in 2015, the company operates an owned manufacturing plant with an area of approximately 10,000 square meters. The facility is equipped with hundreds of machine tools and automated production systems. This combination of equipment and production organization supports repeatable machining, stable output, and the ability to handle both standard products and project-specific requirements.
Process Control from Raw Material to Finished Product
Manufacturing a reliable thread insert requires more than cutting a cylindrical sleeve. The internal thread, external self-tapping profile, three locking holes, length, concentricity, surface condition, and material properties must work together. Process control therefore begins with material verification and continues through forming, machining, inspection, cleaning, packaging, and shipment.
Stainless steel material should be selected according to the required corrosion resistance, strength, hardness, and forming characteristics. Material identification and incoming inspection help ensure that production begins with an appropriate raw material. Correct material control is important because the insert must be strong enough to resist deformation while still allowing the external profile to engage the substrate effectively.
Computer-controlled and automated equipment can improve consistency in turning, threading, grooving, and hole formation. Stable machining parameters help control dimensional variation between batches. Automated production also reduces dependence on manual adjustment for repetitive operations, supporting more consistent geometry and throughput.
Precision of Internal and External Threads
The internal thread must receive the mating bolt accurately and maintain the required load-bearing form. The external thread must match the installation hole and provide controlled cutting or forming action. If either thread is outside tolerance, installation force, alignment, and joint performance may be affected.
Inspection may include thread gauges, dimensional measurement, visual inspection, and sampling of finished parts. For customer-specific programs, inspection plans can be aligned with drawings, technical agreements, and quality requirements. Controlling the relationship between internal and external thread axes is also important because concentricity affects bolt alignment and load distribution.
Control of the Three Locking Features
The three holes or grooves must be distributed evenly around the insert. Their position, size, and depth affect how the base material enters the locking structure. Uneven placement may create an unbalanced installation load or reduce anti-rotation performance.
Production inspection should therefore verify the circumferential distribution and dimensional consistency of these features. A stable process ensures that each insert produces a similar mechanical interlock when installed under the same conditions.
Automated Production and Capacity
The combination of hundreds of machine tools and automated production systems provides a foundation for large-volume supply. In 2024, the company reported an annual output value of approximately RMB 153 million. This scale indicates experience in organizing production, managing multiple product categories, and supporting ongoing supply for industrial customers.
Capacity is valuable not only for large orders but also for continuity. Customers using inserts in production equipment need consistent availability and stable specifications over time. A manufacturer with broad equipment resources can support routine orders, replacement demand, and development projects with greater flexibility than a small workshop focused on a single product.
Traceability and Service Support
Threaded connection products are often used in assemblies where a small component can influence the reliability of a larger system. Consistent labeling, batch management, inspection records, and packaging help customers identify products and control their own manufacturing processes.
Jinzhize emphasizes consistent and traceable products together with after-sales service. Technical communication can cover size selection, installation tools, drilling recommendations, substrate compatibility, packaging, and application concerns. This support is particularly useful when a customer is changing from direct tapping to insert-based reinforcement or developing a new assembly around a soft material.
Advantages Compared with Alternative Thread Reinforcement Methods
Compared with Directly Tapped Threads
A direct tapped hole is simple and economical when the base material is strong enough and the thread will not be repeatedly used. However, it may provide limited strength in aluminum, plastics, wood, and soft castings. The thread can strip under excessive torque or wear after repeated service.
The three-hole insert adds a durable stainless steel internal thread and creates a larger load-transfer interface. It is therefore a stronger option for lightweight or low-strength substrates. The trade-off is that an accurately sized hole and an installation operation are required.
Compared with Smooth Bushings
A smooth bushing can restore diameter or provide a bearing surface, but it does not necessarily create a strong threaded connection or resist rotation. The three-hole insert combines an internal thread with external mechanical locking, giving it a broader fastening function.
Compared with Adhesive-Bonded Inserts
Adhesive-bonded inserts depend heavily on surface preparation, adhesive selection, curing conditions, temperature, chemical compatibility, and long-term bond stability. They may be appropriate in some applications, but production control can be complex.
The three-hole insert relies primarily on mechanical interlocking. This can simplify installation and reduce dependence on curing time. It is also useful where oil, moisture, or production schedules make adhesive processing inconvenient. Adhesive and mechanical methods should be selected according to the actual design requirements rather than treated as universally interchangeable.
Compared with Conventional Press-Fit Inserts
Press-fit inserts typically require a controlled interference relationship between the insert and the hole. Excessive interference can crack a brittle workpiece, while insufficient interference can allow the insert to rotate or pull out. A self-tapping three-hole insert forms its own external engagement and adds discrete locking points, making it adaptable to a range of soft substrates.
Compared with Wire Thread Inserts
Helical wire inserts are excellent for reinforcing internal threads and are widely used in aerospace, automotive, and industrial applications. They usually require a specially tapped installation hole and an insertion process. A three-hole self-tapping insert can be advantageous when the customer wants to avoid forming a separate external thread in the base material.
The two products serve related but different purposes. Wire inserts are often selected for minimal wall thickness, high internal thread performance, and standardized repair systems. Three-hole inserts are attractive when strong external mechanical locking, simple pre-drilled-hole installation, and a solid stainless sleeve are preferred.
Design and Purchasing Considerations
When specifying a three-hole insert, begin with the mating bolt or screw. Confirm the internal thread system, pitch, tolerance, bolt grade, required engagement length, and operating load. Next, identify the base material and determine whether it is aluminum alloy, cast iron, soft steel, plastic, wood, or another substrate.
Consider the minimum wall thickness around the hole. A larger insert can increase thread capacity, but it also removes more base material during drilling. The designer must balance external diameter with remaining wall strength. For blind holes, account for tool clearance, chips, and the minimum drilling depth.
Environmental conditions should guide stainless material selection. Humidity, salt, cleaning agents, temperature, and contact with dissimilar metals can affect the service life of the complete assembly. If the fastener is made from a different metal, galvanic corrosion should be evaluated.
Installation equipment is another important consideration. A production line may require a controlled manual tool, pneumatic equipment, electric equipment, or a custom fixture. The tool should match the insert’s internal thread and provide adequate alignment. Customers should also establish inspection criteria for depth, perpendicularity, torque, and thread condition.
For large or continuing programs, packaging and delivery consistency matter as much as individual part quality. Inserts should be protected from contamination, mixed sizes, mechanical damage, and moisture during storage and transport. Clear labels and batch identification simplify inventory control and quality investigations.
Recommended Quality Verification
A practical inspection program can include several levels of verification. Incoming material checks confirm the stainless steel specification. Dimensional inspection verifies internal thread, external diameter, insert length, locking-hole geometry, and concentricity. Visual inspection identifies burrs, cracks, incomplete threads, surface damage, or contamination.
Installation testing should be performed in representative base materials. The test can evaluate insertion torque, seating depth, thread engagement, torque-out resistance, pull-out resistance, and the condition of the surrounding substrate. These tests should be defined according to the customer’s engineering requirements and the intended service conditions.
Environmental testing may include humidity exposure, salt spray, thermal cycling, chemical contact, and repeated assembly testing. Not every project requires every test, but critical assemblies benefit from validation using the actual insert, substrate, bolt, coating, and installation process.
Quality verification should also examine process capability. If a dimension is important to installation, the manufacturer and customer can identify it as a special characteristic and monitor it more closely. Statistical sampling, calibrated gauges, and documented corrective actions help maintain stable production over time.
Q&A: Common Questions About Three-Hole Thread Inserts
What is the primary purpose of a three-hole thread insert?
Its primary purpose is to create a strong, durable internal thread in a low-strength or easily damaged base material. The three external locking features engage the surrounding material and help prevent rotation and loosening.
Can the insert be used in aluminum?
Yes. Aluminum alloy is one of the main applications for this type of insert. The stainless steel sleeve provides a stronger internal thread than the aluminum substrate alone. The recommended drilling diameter must be selected for the specific insert and aluminum alloy.
Can it be installed in plastic?
It may be suitable for certain plastics, especially where the plastic has enough wall thickness and strength to form a reliable mechanical interlock. Testing is recommended because plastics differ significantly in hardness, elasticity, creep resistance, and temperature performance.
What is the difference between 307 and 308 types?
The supplied product information identifies the 308 type as a reinforced or longer version of the 307 type. The main listed difference is length. The correct selection depends on component thickness, available installation depth, and the required internal thread engagement.
Does the insert eliminate the need for a locking nut or threadlocker?
Not necessarily. The insert resists rotation in the base material, but the complete bolted joint may still require a locking method depending on vibration, preload, safety requirements, and engineering standards. The choice should be based on the complete joint design.
Can a damaged threaded hole be repaired with this product?
In many cases, yes, provided that enough surrounding material remains and the component can accept the required larger hole. The damaged hole must be accurately prepared, and the repaired connection should be inspected after installation.
Is a special installation tool required?
A dedicated installation tool is recommended. It helps align the insert, transmit installation torque, and seat the insert at the correct depth. Using an unsuitable tool can damage the internal thread or cause misalignment.
What should be checked before ordering?
Confirm the internal thread size, pitch, insert length, 307 or 308 type, external thread diameter, base material, drilling diameter, minimum drilling depth, stainless material requirements, and quantity. For production projects, also confirm inspection documents, packaging, delivery schedule, and tool requirements.
Are the listed drilling dimensions universal?
No. The listed dimensions are reference values. Actual drilling requirements may vary according to substrate hardness, hole-making method, tolerance, wall thickness, and installation process. Critical applications should be validated using production-representative samples.
Why choose stainless steel instead of ordinary steel?
Stainless steel generally provides better resistance to rust and corrosion, making it suitable for humid, salty, clean, or chemically exposed environments. It can also provide a durable internal thread for repeated maintenance. The exact performance depends on the stainless grade and the environment.
Why Choose an Experienced Threaded-Connection Manufacturer?
A thread insert is a small component, but its performance depends on precise geometry, correct material, stable machining, and compatible installation practice. An experienced manufacturer can provide more than a standard catalog part. It can help select the correct size, clarify drilling requirements, supply installation tools, and support validation for the customer’s actual substrate.
Dongtai Jinzhize Metal Products Co., Ltd. focuses on threaded connection and fastening products for the global market. Its product portfolio covers several related categories, allowing customers to coordinate self-tapping inserts, wire inserts, key-locking inserts, threaded adapters, oil plugs, taps, and installation equipment through one supplier.
The company’s owned plant, broad machine-tool base, automated production systems, engineering experience, and quality management approach support stable supply. Its products are used in automotive engines and transmissions, commercial vehicles, aerospace manufacturing, rail vehicles, machinery, and other industrial applications. This application background provides useful insight into the requirements of high-strength threaded connections.
For customers, the principal value is a combination of product performance and manufacturing support. A reliable insert must be available in the correct size, produced consistently, packed correctly, and supported by clear technical information. These capabilities help reduce procurement risk, installation errors, rework, and unexpected maintenance problems.
Conclusion
The stainless steel three-hole thread insert is a practical solution for strengthening threaded connections in aluminum, plastic, cast iron, soft steel, wood, and other low-strength substrates. Its internal stainless steel thread provides a durable fastening surface, while the three evenly distributed locking holes create a mechanical interlock that improves anti-rotation and anti-loosening performance.
Its corrosion resistance makes it suitable for humid, high-salt, clean, and industrial environments. Its self-tapping installation process reduces machining steps, and its size range from M3 to M16 supports applications from compact equipment to larger mechanical assemblies. The 307 and 308 options provide flexibility in insert length and engagement depth.
Compared with direct tapping, smooth bushings, adhesive inserts, and some press-fit solutions, the three-hole design offers a strong combination of mechanical locking, repeated-use durability, installation efficiency, and corrosion resistance. Correct selection and installation remain essential. Engineers should verify the substrate, hole diameter, drilling depth, insert length, bolt specification, wall thickness, and environmental requirements.
With specialized manufacturing experience, automated production systems, extensive machine capacity, quality control, and a broad threaded-product portfolio, Dongtai Jinzhize Metal Products Co., Ltd. is positioned to support both standard orders and customized threaded-connection programs. For manufacturers seeking to improve assembly reliability, extend component life, and reduce the risks associated with weak or damaged threaded holes, the stainless steel three-hole insert is a dependable and versatile choice.
References
1. Product specification information for 307 and 308 type three-hole self-tapping thread inserts, including size, length, external thread, drilling diameter, and minimum drilling depth data.
2. General engineering principles for threaded fasteners, thread engagement, torque control, and mechanical joint design.
3. General stainless steel material guidance for corrosion resistance, environmental exposure, and dissimilar-metal considerations.
4. General manufacturing quality-control practices for machined threaded components, dimensional inspection, traceability, and process verification.
5. Company information and manufacturing profile of Dongtai Jinzhize Metal Products Co., Ltd., including product categories, production capabilities, application sectors, and service commitments.
6. General installation principles for self-tapping threaded inserts in aluminum alloys, cast iron, plastics, soft steel, and other low-strength base materials.